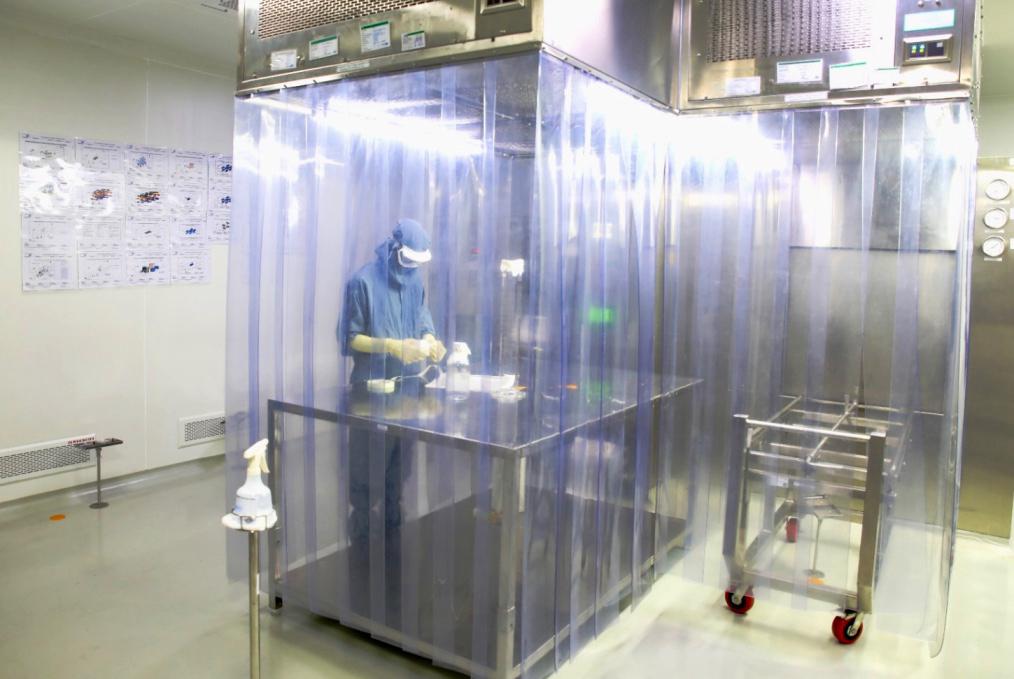
In order for any medicine to be effective it must go through a complex manufacturing process that ensures product safety and quality. And this is where Good Manufacturing Practices play a critical role. Commonly known as Gmp, they are a system of guidelines designed to ensure that products across all industries are consistently manufactured according to established quality standards. For the pharmaceutical industry, it serves as the foundation for quality assurance, helping manufacturers produce medicines that are safe, effective, and of the required quality every time.
GMP works on a simple principle. Instead of relying solely on testing the final product, it incorporates quality checks and regulations into every stage of production. While product testing is an essential part, it alone cannot detect every issue that may have occurred during manufacturing. GMP aims to prevent these problems from occurring through strict controls throughout the production process..
Risk prevention is another major goal of GMP. Pharmaceutical manufacturing involves multiple steps, beginning from sourcing raw materials to packaging finished products. At each stage, there is potential for contamination, cross-contamination, mix-ups, or human error. GMP establishes procedures and controls that help minimize these risks and ensure that products meet the required standards of safety and quality.
One of the major benefits following GMP is maintaining consistency . Patients and healthcare providers expect every batch of a medicine to perform the same way. GMP helps ensure that products manufactured today are identical in quality to those produced months or even years later. This consistency is essential for maintaining patient safety and ensuring confidence in healthcare products.
In a pharmaceutical manufacturing unit GMP measures include clean, well maintained and regularly calibrated facilities and equipment to ensure reliable performance. Employees must receive appropriate training and follow strict hygiene practices to prevent contamination and errors. Comprehensive documentation is required at every stage of production, creating a clear record that supports traceability, accountability, and quality control. In addition, raw materials must be carefully sourced, tested, handled, and stored to ensure they meet established specifications before entering the manufacturing process.
The World Health Organization (WHO) GMP framework is the most recognized standard , which provides internationally accepted guidelines for pharmaceutical manufacturing and quality assurance. The European Union (EU) GMP standards are also regarded as some of the most stringent regulatory requirements globally, focusing on comprehensive quality systems, risk management, and product integrity throughout the manufacturing lifecycle. Similarly, United States GMP regulations, enforced by the U.S. Food and Drug Administration (FDA), establish strict requirements for facilities, processes, documentation, and quality control to ensure pharmaceutical products consistently meet safety and efficacy expectations. Compliance with these internationally recognized GMP standards reflects manufacturer’s commitment to quality, patient safety, and continuous improvement. As products meet the expectations of regulatory authorities worldwide it helps facilitate access to global markets.
GMP is widely referred to as ‘cGMP’, where c represents ‘current’. This emphasizes that manufacturing practices must keep evolving with the development of technology and highlights the need for manufacturers to continuously update their processes and methods to meet evolving quality standards. This approach helps ensure that manufacturing practices keep pace with scientific advancements and regulatory expectations. In an industry where quality directly impacts human health, GMP remains one of the most important pillars of pharmaceutical manufacturing. It is much more than a regulatory requirement, it is a commitment to quality which helps ensure that every product reaching patients meets the highest standards of safety, efficacy, and reliability.